| Target Product | Calcium carbide (CaC₂), typically supplied in controlled lump-size fractions | Product grade, particle size, gas-generation performance and downstream handling determine furnace and crushing requirements. | Define the required CaC₂ purity, size distribution, moisture limit and allowable fines before selecting furnace capacity. |
| Production Capacity | Small or pilot scale: below 10,000 t/year; medium scale: 10,000–50,000 t/year; large scale: above 50,000 t/year | Capacity affects transformer size, electrode arrangement, furnace diameter, cooling demand and material-handling throughput. | Use annual demand, operating days and planned availability to calculate the required continuous output rather than sizing only by nameplate power. |
| Operating Hours | 7,000–8,000 scheduled operating hours per year is a common planning basis for continuous industrial production | Maintenance, electrode changes, refractory work and unplanned stoppages reduce actual productive time. | Include a realistic availability factor, commonly 80%–92%, in the capacity calculation. |
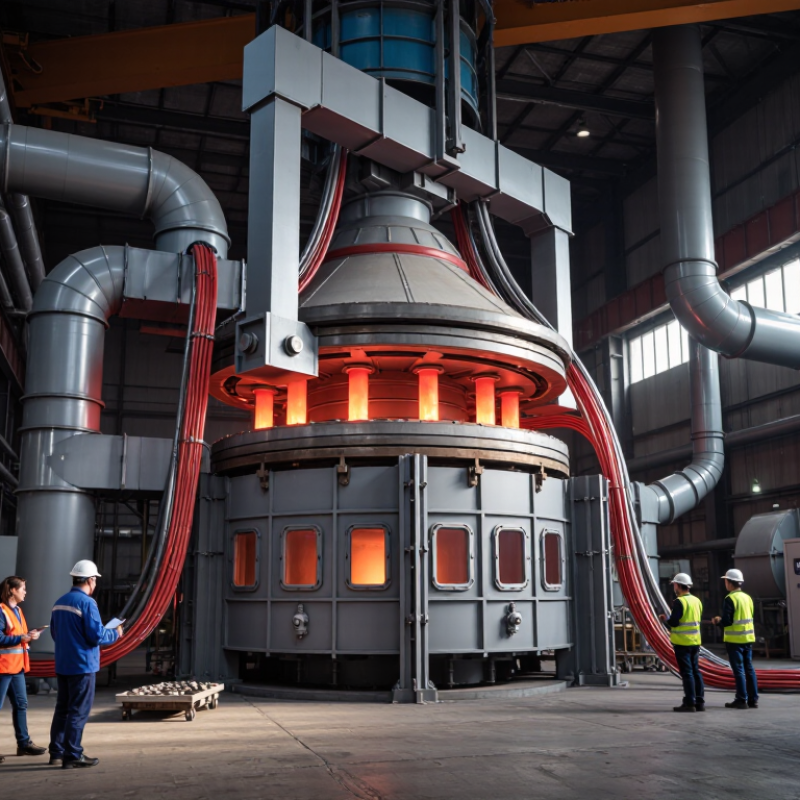
| Furnace Type | Open, semi-closed or closed submerged-arc furnace | The furnace type influences gas capture, environmental control, heat losses, operating complexity and capital cost. | Consider a closed or semi-closed design when carbon monoxide recovery, dust control and emissions management are priorities. |
| Electrical Input | Three-phase AC submerged-arc furnace; industrial installations may range from several MVA to more than 50 MVA | Electrical power is the primary energy source for the high-temperature carbothermic reaction. | Match transformer rating, short-circuit capacity, power quality and grid availability to the furnace operating profile. |
| Specific Energy Consumption | Approximately 3,000–3,500 kWh per metric ton of calcium carbide as an initial engineering benchmark | Actual consumption depends on raw-material quality, furnace efficiency, product grade, operating practice and heat losses. | Request guaranteed performance data based on the same raw materials, product specification and operating conditions. |
| Reaction Temperature | The reaction zone operates at approximately 2,000–2,200°C; the furnace shell and refractory are designed for lower controlled temperatures | High temperature is required for the reaction of quicklime and carbon materials, while containment protects equipment and operators. | Evaluate refractory design, cooling-water protection, thermal monitoring and hot-spot detection. |
| Quicklime Specification | High-calcium quicklime with stable CaO content, low moisture and low levels of silica, iron and magnesium impurities | Impurities consume energy, affect slag formation and can reduce calcium carbide quality. | Set acceptance limits for CaO, SiO₂, Fe₂O₃, MgO, sulfur, moisture and particle-size distribution. |
| Carbon Material Specification | Coke, anthracite or petroleum-coke blends with controlled fixed carbon, ash, volatile matter, sulfur, moisture and electrical resistivity | Carbon reactivity and resistivity influence furnace stability, electrode penetration and energy efficiency. | Use laboratory testing and trial batches to confirm the blend before finalizing electrode and power-control settings. |
| Charge Particle Size | Common feed sizes are roughly 5–50 mm, with the exact range determined by furnace design and material behavior | Uniform burden permeability supports stable gas flow, consistent electrode penetration and predictable electrical resistance. | Specify maximum fines, oversize percentage and moisture variation for each raw material. |
| Electrode System | Three self-baking or prebaked electrodes, selected according to furnace power and current density | Electrode diameter, current capacity, paste quality and regulation accuracy directly affect electrical stability and operating cost. | Compare electrode consumption, slip control, paste-baking performance, breakage protection and spare-part availability. |
| Furnace Regulation | Automatic electrode-position control, transformer tap control and real-time current, voltage and power monitoring | Stable regulation improves reaction-zone control, reduces electrical disturbances and limits electrode incidents. | Require trend recording, alarm management, interlocks and manual override for safe operation. |
| Gas and Dust Management | Gas-tight hood or controlled extraction system with dust collection, carbon-monoxide monitoring and safe flaring or recovery | Calcium carbide furnaces can generate carbon monoxide and particulate emissions that require engineered control. | Design the gas system around local emission limits, gas composition, pressure control and emergency ventilation requirements. |
| Cooling System | Closed-loop water cooling with flow, pressure, temperature and leak detection | Cooling protects the furnace shell, electrode holders, cables and other water-cooled components. | Specify water quality, redundancy, emergency backup and automatic shutdown logic. |
| Product Quality Target | Common commercial grades may target approximately 75%–85% available CaC₂, depending on application and test method | Available calcium carbide is commonly evaluated by the acetylene yield obtained during controlled reaction with water. | Define the test method, sampling procedure, size fraction and acceptance limits in the purchase specification. |
| Acetylene Yield Reference | The theoretical yield is approximately 380 L of acetylene per kilogram of pure CaC₂ at 0°C and 101.325 kPa; commercial yield is lower | This provides a practical reference for checking carbide reactivity and available-CaC₂ performance. | Do not compare yield figures without confirming temperature, pressure, moisture correction and analytical method. |
| Material Balance | The simplified reaction is CaO + 3C → CaC₂ + CO; actual consumption includes impurities, moisture, dust and process losses | Material balance determines raw-material storage, feeding equipment, off-gas handling and waste capacity. | Base the design on tested raw materials and include operating margins for quality variation and start-up losses. |
| Automation and Data | PLC or DCS control with historian functions for power, electrode position, feed rate, cooling, gas pressure and alarms | Reliable operating data supports energy optimization, preventive maintenance and product-quality traceability. | Require open communication protocols, role-based access, backup procedures and cybersecurity controls. |
| Safety Requirements | Interlocks for cooling loss, gas alarms, electrode faults, overcurrent, furnace pressure and emergency shutdown | The process combines high electrical energy, extreme temperatures, molten material, carbon monoxide and reactive carbide. | Complete a site-specific hazard assessment and verify compliance with applicable electrical, pressure, fire and occupational-safety rules. |
| Lifecycle Evaluation | Compare total cost of ownership, not only initial furnace price | Electricity, electrodes, refractory, cooling water, maintenance, dust disposal, downtime and labor can dominate long-term cost. | Request a documented five-to-ten-year operating-cost model with assumptions for energy price, production rate and maintenance intervals. |